World Leader in Moisture Measurement & Control. Using near-infrared technology, we can provide 100% product inspection instantly on the production line.
In animal feed production, moisture variation can affect pellet quality, yield, energy use and production stability. Real-time moisture measurement helps operators identify changes sooner and keep production closer to target.
🔗 https://t.co/67ORyWuvwx
#AnimalFeed
When moisture varies, the entire paperboard process can feel the effects. In this paperboard application, MoistTech's online moisture measurement provided the plant with real-time process visibility without interrupting production.
https://t.co/m4fYsUIXHW
#PaperManufacturing
Lab testing tells you what happened. Online measurement helps you control what is happening now. Use real-time moisture data to improve bonding, flatness, and converting consistency. https://t.co/3aKvY323iC
See if online moisture measurement is right for your process.
Small variations become big problems fast on a high-speed line. In corrugated and linerboard production, changes in moisture or coat weight can affect web consistency, drying performance, bonding and finished product quality. 🔗 https://t.co/NGpUMoxKcK #Corrugated#ProcessControl
MoistTech looks forward to connecting with processing professionals at POWTECH in Nuremberg, Germany September 23-25! Visit us to discuss how continuous, real-time moisture measurement can help support more consistent quality. https://t.co/5GE6qcF8QW
#POWTECH#ProcessTechnology
We’re headed to Dortmund! 🇩🇪 #InterTabac is almost underway, and MoistTech is excited to showcase real-time moisture measurement solutions for the tobacco industry.
📍 Dortmund, Germany
📅 September 15–17
We look forward to seeing you there!
🔗 https://t.co/1kDTZ77euC
In a recent Paper Film & Foil Converter article, MoistTech explores how continuous, real-time moisture data can help reduce energy use, minimize waste, improve yield, and support proactive process control.
Read the full article: https://t.co/a7lcNYIput
Move beyond reacting to moisture variability. With continuous, real-time measurement, manufacturers can make proactive process adjustments, strengthen quality control, and maintain more consistent production.
Discover how: https://t.co/pKOdTQFqYN
#MoistTech#MoistureSensors
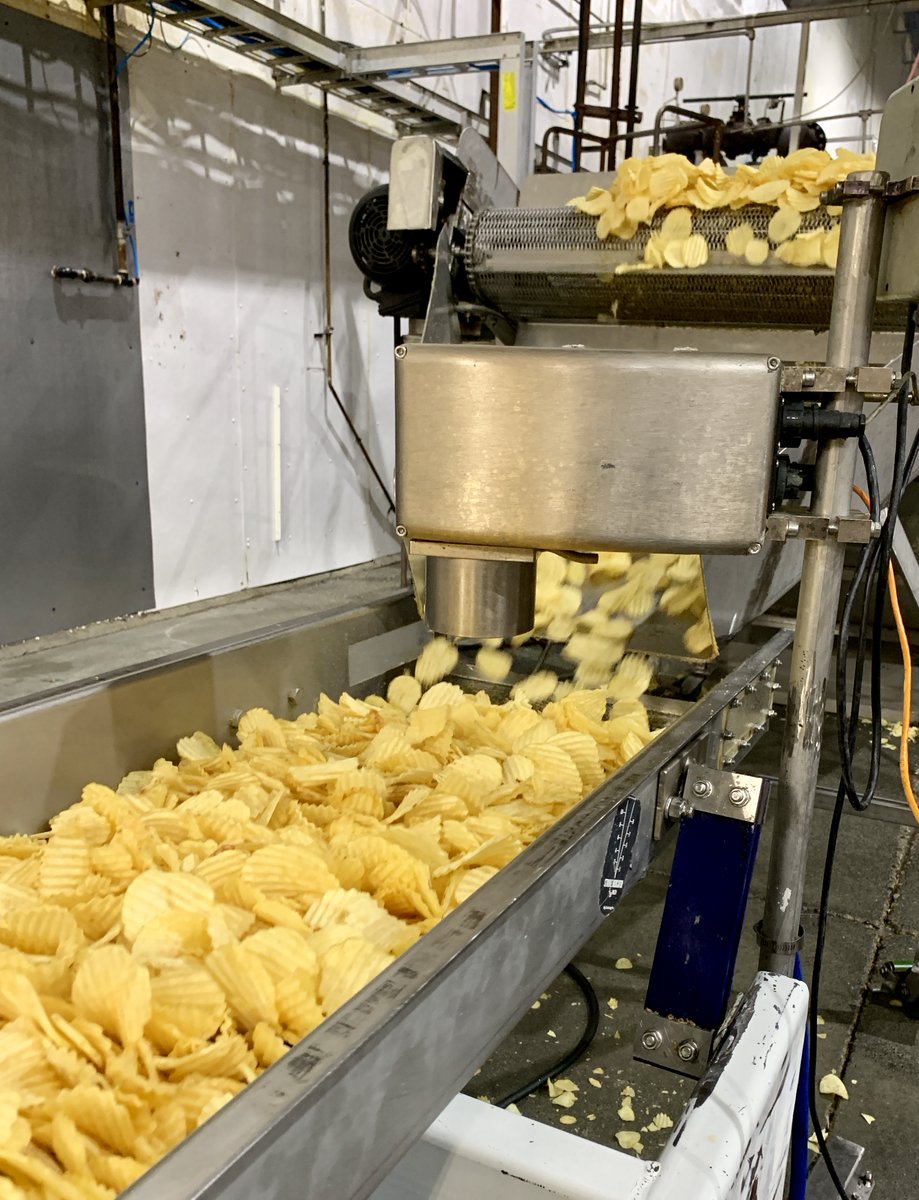
#SnackFoods demand consistency, from crunchy popcorn to perfectly roasted nuts. MoistTech’s advanced #Moisture sensors help manufacturers monitor moisture in real time to support product quality, reduce waste, and keep production on target.
Learn more: https://t.co/OZjKBiKtw7
MoistTech’s online NIR sensors put accurate, real-time data into your PLC or SCADA system, reducing manual sampling and freeing operators to handle higher-value tasks. The result is fewer surprises, faster adjustments, and more consistent product quality.
https://t.co/pVLIs62dlH
Meeting sustainability and energy reduction targets starts with knowing moisture in real time. MoistTech’s IR‑3000 sensor helps plants tune dryers, reduce over‑processing, and avoid scrap, supporting both cost savings and ESG initiatives.
#SustainableManufacturing#EnergySavings
In bioenergy and biomass operations, moisture measurement drives efficiency and consistency. MoistTech’s IR-3000 sensors give operators a view of moisture across feedstock and fuel streams, helping cut downtime and improve energy yield.https://t.co/DnfbGf1qMV
#BioEnergy#Biomass
MoistTech’s 868 Laboratory NIR sensor and IRMA 858 provide rapid moisture readings in seconds with sealed dishes or jars. https://t.co/pmA5mgmsZL
#LabTesting#NIRAnalyzer#QualityControl
By reducing energy consumption, scrap, and manual testing, #MoistTech’s moisture sensors can deliver rapid #ROI while supporting sustainability initiatives. Many manufacturers see measurable savings in energy and materials when they use real‑time NIR data. https://t.co/pVLIs62dlH
In #Mineral processing, moisture impacts dryer performance, dust control, and product quality across bulk solids. MoistTech’s IR‑3000 series sensors provide continuous moisture readings that help operations boost dryer efficiency, improve safety, and reduce off‑spec shipments.
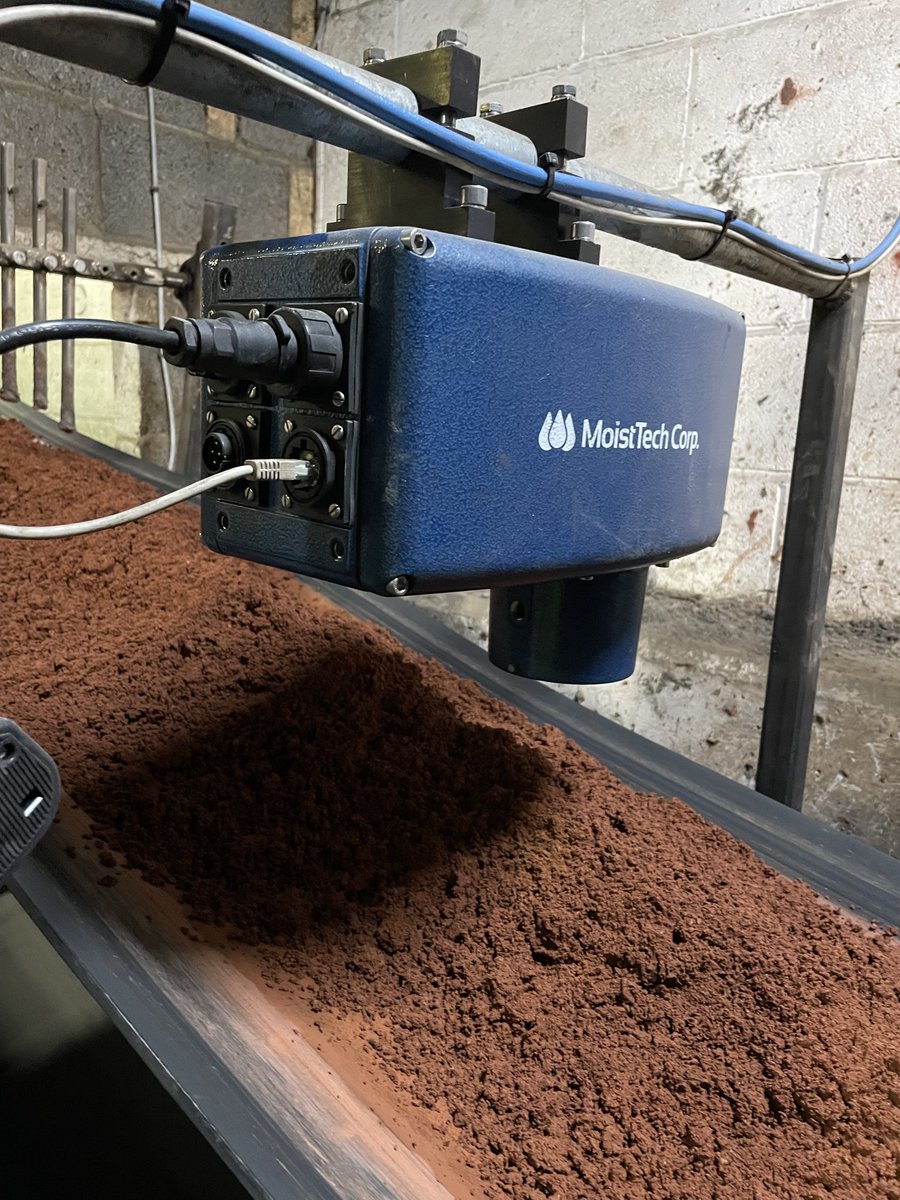
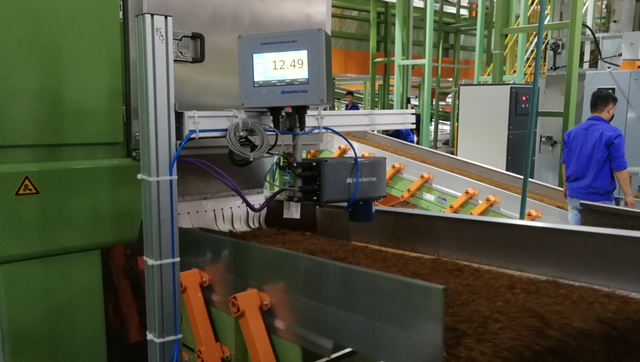
The 828 tobacco sensor is engineered specifically for demanding tobacco processes, providing instant, non-contact NIR moisture readings for expanded, cut, leaf, and reconstituted tobacco.
#TobaccoMoisture#ProcessControl
Consistent tobacco moisture is essential for quality, compliance, and processing efficiency from leaf to finished product. MoistTech’s tobacco moisture solutions deliver continuous, non-contact measurements within tight tolerances.
#TobaccoIndustry#MoistureControl
A leading food manufacturer improved quality and reduced downtime by replacing periodic lab tests with MoistTech’s online IR-3000 sensors. Real-time NIR data stabilized dryer settings, reduced waste, and delivered energy savings.
#FoodManufacturing#MoistureMeasurement