I ran across this video a few days ago and couldn’t stop watching it.
It’s about something ordinary & boring, a plastic gas lighter. But it changes how one thinks about manufacturing.
That lighter in so many of our homes, holds pressurised gas. It has over 30 microscopic parts, has to pass international safety codes, & travel 10,000 miles by sea, & the total cost of doing all that, materials, labour, freight, every middleman along the way, comes to fifteen U.S cents.
So how does anyone make money on this?
Turns out almost the entire world’s supply comes from one place: a county called Shaodong, in China’s Hunan province.
It wasn’t always there.
But today, Shaodong has 114 lighter-related companies packed into the place & between them they source more than 200 different components from each other, all within a 20-kilometre radius. They supply something like seventy percent of the world’s disposable lighters. And the industry alone employs over 80,000 people locally.
Nobody there is winning on cheap labour anymore. They’re winning by shaving a thousandth of a cent off the thickness of a plastic wall, or redesigning a base so a few thousand more units fit into the same shipping container.
It took my thoughts back to an old professor of mine, Michael Porter.
His 1980 book, Competitive Strategy, is still the 1st book most MBAs read, the one that gave the world the Five Forces and basically invented modern strategic thinking.
But there’s a quieter piece of his work, on industrial clusters, that never got nearly the same attention, and it is the one that explains exactly what is happening in Shaodong.
His argument was that nations and regions rarely win because of cheap inputs. They win when rival firms and specialist suppliers crowd into the same small geography for long enough that they keep pushing each other past what any one of them could manage alone. He found it in the Swiss watchmaking towns of the Jura, in the German printing press industry and in Italy’s ceramic tile and footwear districts (interestingly, it’s the SAME blueprint which built Morbi, in Gujarat, into the world’s second-largest ceramic cluster, now outproducing Italy by volume. I have posted before, about Morbi)
None of these started out as giants. The neighbourhood made them giants.
Which is exactly why it’s so relevant to India’s climb up the global manufacturing table
I’ve also attached a slide with this post that I saw recently and which shows us breaking into the top 5 manufacturing globally. (A quick reference check told me that we may not have overtaken Korea yet, but the trajectory’s clear)
That climb has happened on the back of scale: bigger plants, bigger parks, more FDI.
I should declare an interest here, because the Mahindra Group set up 2 of India’s first integrated, plug-and-play business cities, in Chennai in 2002 & Jaipur in 2006.
Both have been extremely successful. Chennai’s business zone alone today employs 45,000 people..
But I admit that we need to think differently.
A park brings in investors and hands them a ready plot, power, water & roads
A cluster is a completely different animal: hundreds of small, specialised suppliers, each obsessed with doing a tiny thing better than anyone else, feeding off each other’s presence for years until no outsider can compete with the whole.
I think that’s the work ahead of us now.
Not just more factories, and not just more parks.
Policymakers & developers like us need to start consciously pulling as many of the inputs and resources a sector needs, the toolmakers, the component suppliers, the testing labs, the logistics specialists, into the same neighbourhood.
Shaodong and Morbi both got there by accident, one town stumbling onto a way to shave a thousandth of a cent off a lighter wall, the other discovering it had the clay and, later, the gas pipeline for tiles.
We don’t have the luxury of waiting for accidents anymore.
We need to do it on purpose
"Make it cheaper."
If you've been in manufacturing, you've heard those words 1000s of times.
That's how a lot of products are made.
- Take something good
- Remove features
- Reduce quality
- Hope nobody notices
We decided to do the EXACT OPPOSITE.
Instead of asking how cheap we could make it, we asked:
"How GREAT can we make it?"
We blindly invested in moulds.
We made it better in every way we could.
It was a big risk.
We had no idea if customers would pay for it.
But we believed something simple:
Indians deserve great products too.
Then we met the founders of @curaahome:
@rajshamani, @SanjyotKeer & @NeerajUdai.
And from the first conversation, it felt different.
Most brands ask manufacturers how much cost they can remove.
Cüraa asked how much value we could ADD.
That changed everything.
Today, that hand mixer is live.
The most premium hand mixer Made in Bharat.
Premium because nobody involved wanted to compromise.
When more brands & manufacturers are willing to take bets on quality,
India starts building products that matter.
Want to buy?
Link in the first comment.
Indeed, it was *because* I was not from the aerospace industry that SpaceX made such radical breakthroughs. Same for Tesla.
Those in the industry would have if they could have.
I’m thrilled to announce we’ve raised $44M to build a new home for product design. Meet @noondesign.
No workflow is more broken and fragmented in 2026 than the product designers’. The very same people who care most about building software don’t have software purpose built for them. @kushagrasinha7 and I have lived this problem first hand as designers ourselves.
That’s why we built Noon. The first product design tool that works entirely on your product code, so you can design not only how a product looks, but also how it works. With AI at its core that works in seconds, not minutes.
For the first time, you can create, iterate, build, test and ship. All in one canvas. No translations or roundtrips to the codebase and back.
Comment “Get Noon” and we’ll get you on the list for early access.
BREAKING 🚨 @Tesla HAS ENGINEERED A SYNCHRONIZED MULTI-ROLL CALENDERING MACHINE THAT USES DIFFERENTIAL ROLLER SPEEDS TO EFFORTLESSLY TURN DELICATE DRY POWDERS INTO CONTINUOUS BATTERY ELECTRODES 🔋
For years, mastering the "dry battery electrode" has been the holy grail of Tesla's manufacturing roadmap. The promise was always massive: eliminate the toxic, energy-guzzling drying ovens used in traditional battery making, drastically shrink the factory footprint, and slash production costs.
But handling delicate, dry chemical powders at industrial speeds has proven incredibly difficult. Early attempts relied on brute force, crushing the powders with immense pressure just to get them to stick together—a process that was hard on both the machinery and the materials.
Now, it appears Tesla has finally cracked the code, replacing that destructive pressure with an elegant mechanical dance.
The secret to this manufacturing breakthrough lies in rotational physics rather than brute force. By programming each successive roller in their new lamination machine to spin slightly faster than the one behind it, Tesla creates a gentle shear force that pulls the dry powder along.
This clever manipulation of speed eliminates the need for the massive pressures and thick, free-standing films that previously held back dry battery manufacturing.
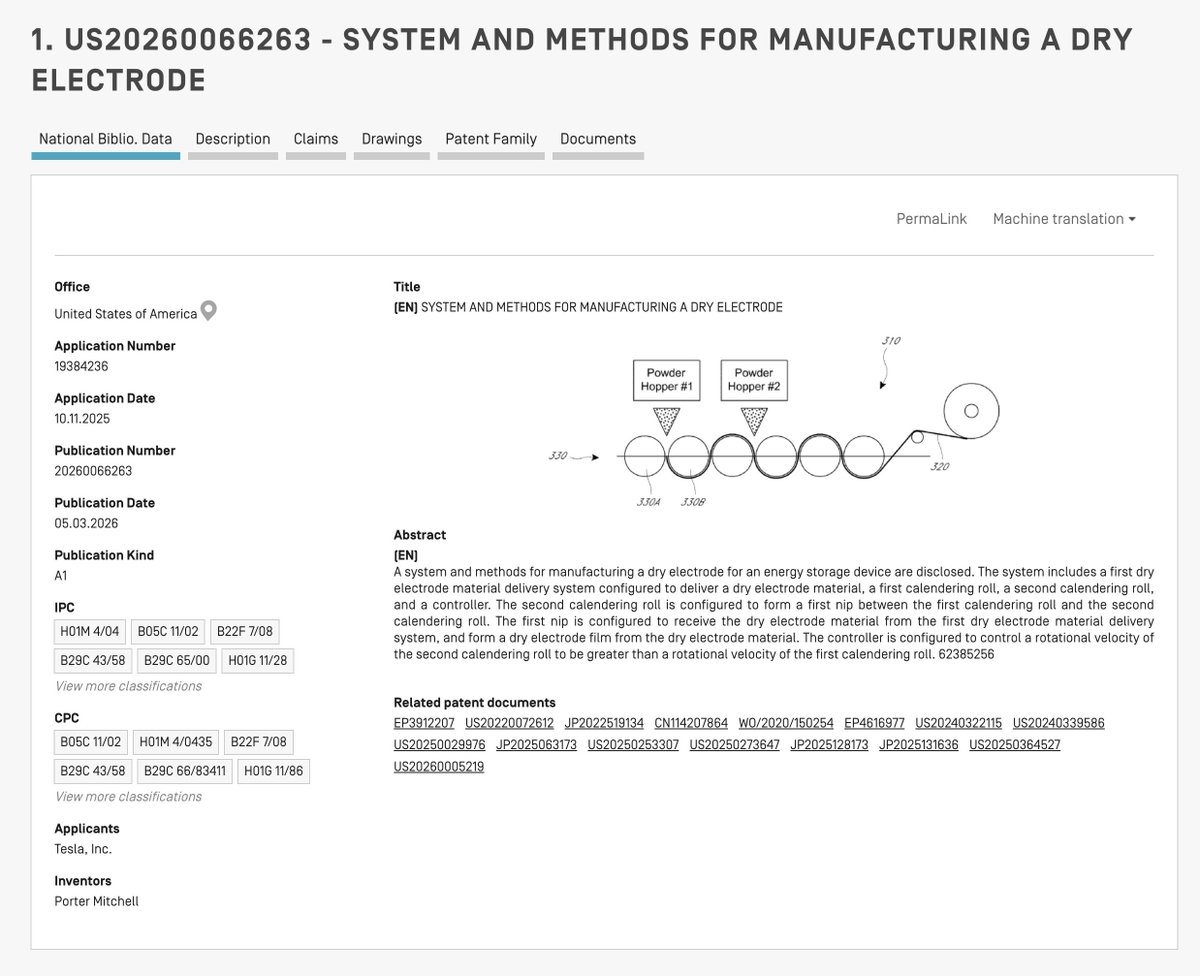
These exact mechanics are laid out in patent US20260066263A1, which was published on March 5, 2026, under the title "System and methods for manufacturing a dry electrode." This document gives us an unprecedented look at how the company intends to scale up its next-generation energy storage products without relying on outdated wet processes.
Instead of depending on toxic liquid slurries or giant drying ovens, the new system handles free-flowing particles with remarkable grace. The machine supports the fragile powder film entirely on the rollers themselves from start to finish.
This delicate touch is exactly what allows them to seamlessly process advanced, air-sensitive chemistries directly onto metal foils. To understand why this shift is so significant, we first have to look at the messy, expensive hurdles that have defined battery making for decades.
⚖️ The problem: Overcoming the limits of traditional electrode manufacturing
Battery manufacturing has historically relied on wet processes. These traditional methods require mixing active materials, which are the core chemical ingredients that actually store and release electrical energy, with toxic liquid solvents.
This mixing creates a wet, thick batter known as a slurry. The slurry is then coated onto a metal foil, a thin conductive sheet that acts as the backbone of the battery to collect the electricity.
After coating, this wet layer must be passed through massive drying ovens to evaporate the liquids. This entire baking step consumes immense amounts of energy and takes up a huge amount of factory floor space.
Dry electrode manufacturing attempts to solve this massive inefficiency by removing the liquids entirely. Older dry processing systems tried to achieve this by using heavy pressure and exceptionally high shear, which is an intense frictional rubbing or smearing force similar to aggressively spreading cold butter on delicate bread.
These extreme forces were needed to pack the dry powders into a cohesive film, meaning a solid, continuous sheet of material that tightly holds itself together. The resulting film then had to be physically strong enough to support its own weight as it floated and moved across the gaps in the machinery.
Building a machine to handle these intense pressures while keeping the fragile, unsupported film intact proved to be highly complex and prohibitively expensive. This is exactly where Tesla’s new architecture steps in, replacing brute force with a far more sophisticated mechanical dance.
💡 Tesla's solution: A synchronized multi-roll calendering architecture
Tesla designed a specialized calendering machine, which is essentially a heavy pressing device that flattens materials much like an industrial pasta maker. This architecture uses multiple rollers arranged in a continuous sequence.
Instead of forcing the dry powder into a standalone sheet that has to hang freely in the air, the system feeds the raw dry powder directly into the first set of rollers.
The true innovation of this design lies in how the machine controls the speed of these rotating cylinders. Every subsequent roller in the sequence is programmed to rotate slightly faster than the one right before it.
This deliberate speed difference creates a gentle shear force within the powder mixture. We can think of this shear force as a mild stretching and aligning action, very similar to how a baker gently stretches dough to make it perfectly smooth.
This gentle pulling action causes the newly formed dry film to naturally adhere to the faster moving roller, making it cling to the metal surface almost like a magnet.
The film simply rides along the solid surface of the rollers through the entire machine rather than floating across open gaps. Because the delicate film is constantly supported by the steel rollers beneath it, it never has to be structurally strong enough to support its own weight. By keeping the material anchored to the rollers, Tesla was able to strip away layers of unnecessary hardware that previously cluttered the production line.
⚙️ Mechanical simplicity: Removing idler rolls, reducing pressure, and adding heat
Older machines required numerous idler rolls, which are unpowered cylinders that simply help route materials along a path, and dancer rolls. We can think of dancer rolls as weighted movable pulleys that bob up and down to maintain a constant tension on a moving web.
These extra components were necessary to guide the fragile and unsupported film through the open air from one processing section to the next. The Tesla design completely eliminates the need for these extra guiding wheels.
The film simply passes directly from one nip point, the tight pinching area where two heavy rollers meet to squeeze the material together, straight to the next.
The brilliance of Tesla's multi-roll system is also its modularity. The architecture isn't fixed. The machine can be configured with anywhere from three rolls creating two pinch points up to seven rolls creating six pinch points, depending on the exact thickness and density required for a specific battery chemistry.
Furthermore, it is not just about physical pressure and speed. It is also about heat. The system allows for precise, independent temperature control for every single roller. The final roller in the stack, for example, can be heated to a specific degree to assist with the final lamination. It isn't just mashing the powder onto the foil. It is creating a permanent thermo-mechanical bond.
Because the equipment does not have to fight against the weakness of a free floating film, the machinery requires much lower pressures to compress the powder to the desired thickness. The equipment can therefore be built smaller and lighter while still achieving high precision tolerances, meaning the exact microscopic accuracy required for the final battery electrode to function safely and efficiently. However, even the most advanced rollers cannot perform miracles on plain dust.
To achieve this level of precision, the raw material itself must be fundamentally engineered to hold together under this gentle pressure.
🌪️ The invisible spiderweb: Dry fibrillization
Before the powder ever reaches the machine to begin this rolling process, it undergoes a crucial physical transformation. According to the patent, the raw battery ingredients are first fed through a high-shear device.
This is a powerful machine, such as a jet-mill, which uses high-speed streams of air or intense friction to violently crash particles into one another. The mixture fed into this mill includes the energy-storing active materials, the conductive particles that help electricity flow smoothly through the battery, and the dry binders. These binders act as a powdered chemical glue designed to hold the entire structure together.
This intense pre-mixing step physically stretches those dry binder particles. The intense friction forces them to unravel and form a microscopic matrix of thin, web-like fibers. We can think of this process like pulling a dense cube of sugar into fluffy, interlocking strands of cotton candy. This sticky, fibrillized network is the secret sauce that successfully holds the active battery materials together without needing a single drop of toxic liquid solvent.
When this spiderweb powder finally hits the rollers, the machine is not just compressing loose sand. It is flattening a cohesive, interconnected structural matrix that is already clinging to itself. Handling this delicate and sticky web of powder requires extreme care, as uneven dumping will cause clumps that ruin the precise tolerances of the final battery.
🎛️ Mastering powder flow: The funnel shaped charging hopper
To manage this tricky material, the physical journey into the machine begins at a highly specific funnel shaped charging hopper. This component is essentially a large storage reservoir used to hold and continuously dispense the fibrillized mixture without destroying its delicate web-like structure.
This container is designed to maintain a perfectly constant level of bulk material. A rotary metering roller sits at the bottom of this hopper. This spinning cylindrical tool acts much like a water wheel portioning out equal scoops of water, and it is equipped with small indented pockets called cells that are sized exactly to the microscopic grain size of the powder.
As the roller turns, a flexible doctor blade strips the powder precisely. We can think of this thin and flat scraping tool acting just like a baker using a straight edge to level off a measuring cup of flour so the amount is absolutely perfect.
The measured powder is then conveyed to an oscillating brushing device, a specialized brush that rapidly swings back and forth to distribute the mixture.
This meticulous brushing process ensures the powder is perfectly uniform. It completely avoids any cavity formation, meaning unwanted empty air pockets or uneven clumps, and prevents material decomposition before it even touches the moving conveyor surface.
Once this uniform layer is established, Tesla deploys high-tech sensors to ensure that every single micron of the material meets their rigorous standards.
🔬 High precision hardware: Gamma gauges and playless bearings
Controlling a fragile powder film across multiple rotating cylinders requires immense mechanical precision. The text reveals the integration of Gamma gauges.
These are highly advanced sensors that use safe levels of radiation to peer through the material, much like a medical X-ray checks for bone density. They constantly monitor the film thickness and specific mass, meaning the exact weight and concentration of the powder packed into a given area, as it is being manufactured in real time.
To maintain these incredibly tight tolerances required for high density battery electrodes, the calendering rollers are fixed in a unique position. They use playless conical bearings.
We can think of these specialized tapered mounts as perfectly snug sockets that completely eliminate any wobbling or vibration in the heavy spinning cylinders.
The faces of these individual rolls can also be customized with hard face ceramic or chrome coatings. They can even be patterned as an embossing roll, a textured stamp that presses a permanent physical pattern into the material, to impart specific textures directly to the electrode surface. This level of microscopic control is impressive on its own, but it becomes truly transformative when the machine has to handle complex, non-continuous patterns on the fly.
🗜️ Intelligent lamination: Solving the intermittent coating challenge
Modern battery designs often require intermittent electrodes. These are essentially strips of foil where the active battery material is applied in separated patches, leaving blank spaces of bare metal in between.
We can picture this layout like the dashed white lines painted down the center of a highway. These bare spaces are absolutely necessary for attaching electrical tabs, the small conductive metal strips that act as bridges to carry the electrical current out of the battery cell and into the device.
Laminating these patchy films creates a severe mechanical issue. The lamination rollers, which are massive spinning cylinders that bond the layers together much like an industrial strength sticker machine, exert immense force.
When these heavy rollers suddenly reach a blank gap in the powder coating, the sudden lack of thickness causes the heavy metal to slam violently together. This aggressive slamming not only damages the expensive machine over time but also easily tears the delicate metal foil.
To solve this destructive problem, Tesla integrated intelligent gap control actuators into the laminator. We can think of these actuators as lightning fast mechanical pistons or shock absorbers that can precisely push back against the machinery. Sensors carefully monitor the moving web and detect exactly when a blank uncoated area is approaching the rollers. The central computer controller then instantly engages these opposing actuators to perfectly counteract the heavy crushing force normally used to stick the layers together. This rapid adjustment maintains a perfect and constant gap between the rollers so they can glide smoothly over the bare foil without making any destructive contact.
But avoiding a violent collision is only half the battle; what happens to the continuous sheet of powder when the rollers lift up? The patent outlines a specific "peeling" mechanism. The machine actively peels the un-laminated powder film away from the bare metal current collector. By utilizing a doctor blade to assist in peeling away this waste material, the machine leaves behind perfectly clean, bare metal gaps for the electrical tabs while the un-bonded powder can potentially be recycled back into the system.
🕸️ Automated material handling: Self webbing belts and on the fly adhesives
Tesla has built automated material handling directly into the machinery to reduce factory operator intervention. This means the equipment moves and manages the delicate battery components entirely on its own, greatly reducing the need for human workers to manually adjust the line.
The system can be designed to be completely self webbing, which is a clever mechanical trick where the machine basically threads itself. We can think of this like a modern sewing machine that automatically pulls the thread exactly where it needs to go without requiring a steady hand.
A continuous belt, essentially a long looping conveyor, runs under the rolls. This belt actually rises up during the delicate startup process of stringing the material through the equipment to automatically guide the fragile powder layer in the proper direction toward the next roll nip.
If the electrode formulation requires a binder, which is a chemical glue used to hold the active energy storing particles together, the machine features an entirely separate powder hopper.
This dedicated storage bin can apply adhesive directly to one side of the film on the fly, meaning it adds the glue while the materials are actively moving at full production speed.
This neat addition completely eliminates the separate manufacturing step of pre coating the metal current collector foils with adhesive before they even enter the machine. By consolidating these disparate steps, Tesla has managed to turn an entire factory wing’s worth of equipment into a single, sleek production unit.
🏭 Factory optimization: Consolidating the production line
The physical layout and structural design of the equipment allows Tesla to align two powder delivery systems on the exact same machine. We can think of these delivery systems as giant and precisely calibrated spice shakers that constantly sprinkle the active battery ingredients.
One hopper feeds the top roller and another feeds the bottom roller, while a central copper or aluminum foil is fed directly through the middle of the spinning cylinders.
The machine compresses both dry films and bonds them to both sides of the metal foil at the exact same time. This bonding process acts like a massive mechanical sandwich press that firmly sticks the active ingredients to the metal core.
It combines the calendering, laminating, and slitting steps into a single continuous action. Calendering tightly flattens the powder into a precise thickness, laminating permanently glues those flattened layers to the foil, and slitting finally cuts the wide master sheet into the narrow strips needed to assemble individual battery cells.
This streamlined flow does more than just save space; it provides the precise environment needed to work with the volatile and experimental chemistries of the future.
🚀 The strategic masterstroke: Securing Tesla’s present and future
The key invention of this patent—the continuous multi-roll calendering machine utilizing differential roller speeds—directly solves Tesla's immediate manufacturing bottlenecks. By entirely eliminating the massive and energy-hungry drying ovens required for wet battery slurries, Tesla can drastically shrink the physical footprint of its factories today. This consolidation translates to significantly lower capital expenditures and reduced operating costs, ultimately driving down the sticker price of their electric vehicles and heavy-duty energy storage systems.
But looking toward the future, this low-force lamination technique is what secures Tesla's position at the forefront of next-generation energy storage. Because the gentle rolling process does not crush delicate chemical structures, engineers can seamlessly transition these exact production lines to advanced, highly sensitive chemistries. This opens the door to energy-dense lithium metal powders, high-capacity silicon oxides, molten sulfur, and even solid-state electrolytes. Building this physical grid using a completely dry process allows engineers to finally move beyond traditional lithium-ion constraints, paving the way for vehicles that charge faster and drive much further on a single plug.
Furthermore, producing lighter and more energy-dense power sources is absolutely critical for untethered applications beyond passenger cars. High-performance dry electrodes will be the exact technology needed to power advanced humanoid robots, allowing machines like Optimus to operate for full work shifts without a bulky battery pack. It is also a foundational requirement for aerospace innovations, advanced satellite networks, and orbital technologies.
The implications of this patent even stretch beyond energy storage entirely. The ability to continuously print high-density, porous films without using toxic wet solvents is a holy grail for several other massive industries. The patent explicitly notes that this exact machinery can be used to manufacture ultracapacitors, hydrogen fuel cell components, and even water purification electrodes, potentially lowering the cost of industrial water desalination worldwide.
By mastering this fundamental manufacturing step through clever rotational physics, Tesla isn't just improving car batteries; they are building the exact power foundation required to electrify the broader economy and support the next decade of advanced engineering.
How many π digits do we need?
3.1415 ➡️ design the finest engines
3.1415926535 ➡️ obtain the circumference of the Earth within a fraction of an inch
3.1415926535897932384626433832795028842 ➡️ measure the radius of the universe to an accuracy equal to the size of a hydrogen atom
Attribution is Overrated
Incrementality is What Really Matters
Every new-age founder wants to know: Which channel is working? What’s my ROAS? What’s the CAC by cohort?
All fair questions. But here’s the uncomfortable truth:
Attribution only tells you who got credit.
Incrementality tells you who deserves it.
And if you’re an omnichannel brand, attribution is broken by default. Sales don’t always happen on D2C. People discover you online, but buy on Amazon. Or at Croma. Or at a retail counter 3 days later
You could have an ad that influences the purchase—without owning it in the funnel
Which means you can be making the right marketing decisions, but killing them because they don’t “show up” in your performance dashboard
So what should you do?
Most marketers will say: “Build a marketing mix model.”
But that’s not realistic for 95% of brands under ₹200 Cr in revenue. Too much data dependency. Too much statistical overkill. Too little actionability
Here are 4 ways you can directionally measure incrementality—without needing a data science team or an MMM dashboard
We’ve used these extensively at Atomberg, and I’ve seen other breakout brands do it well
1. Geo Split Testing (Still the best starting point)
Pick 2 similar states or cities. Run a campaign only in one of them
Example: Run Meta and YouTube ads in Gujarat, but not in Maharashtra. Keep distribution and trade inputs constant
Now track 3 things in Gujarat vs Maharashtra:
• Branded search growth
• Sell-through velocity on marketplaces
• Offline secondary sales and counter-level repeat billing
If Gujarat grows disproportionately, you know your campaign had impact. No dashboards needed. Just clean thinking and discipline
2. First-Time Buyer Growth vs Returning Buyer Growth
Your campaign performance might look the same every month. Same ROAS, same CVR, same CAC
But behind that, ask: How much of this is coming from new buyers?
If you’re seeing a rise in first-time customers (across Amazon, D2C), you’re creating new demand
Because loyalists will come back anyway. CRM and brand affinity will do the job. But converting new buyers—that’s where your marketing should be measured
Compare campaigns or months by first-time buyer contribution. That’s your directionally incremental signal
3. Paid Traffic vs Organic Trend Lines
Look at how your organic traffic and sales are moving in relation to paid traffic and sales
If you pump up paid, and see no change in organic branded search, organic orders, or category rankings—that’s a red flag.
Your ads are probably just capturing demand that would’ve come anyway
But if organic metrics go up in parallel with paid activity, that’s a strong sign of spillover impact. It suggests that your paid campaigns are creating new interest, not just closing existing interest
4. Channel Crossover + Offline Signal Mapping (Our favorite play at Atomberg)
Here’s where most brands give up:
“My Meta ads don’t show up in attribution—but I know people are seeing them before buying offline.”
So how do you prove it?
One way is post-purchase surveys (“Where did you first hear about us?”). Good for qualitative data
But we took it a step further
At Atomberg, we pass back installation and warranty registration data into Meta. And it gets mapped back to user level cookies
So if someone saw a Meta ad, clicked, purchased from somewhere else and then registered a product warranty 7 days later, we know which campaign nudged that sale—even if attribution said nothing
This has helped us measure true incrementality. And it’s one of the most powerful ways to validate performance marketing’s offline impact—especially in high-consideration categories
If your business is omnichannel and your product is evaluated, pure attribution will always lie to you
Instead of chasing perfect dashboards, chase directional truth
This mindset won’t win you awards. But it will save you crores
Elon Musk in 2012:
“I love manufacturing. Building solid objects that deliver value to people is really a great thing. I think we should do more of that in this country.”
@scale_kartik@rajshamani@ifeelblanko Hello Kartik, Please share the details on DM and will tell my team to immediately look into it and resolve it on priority!